1.Types of drill bit:
ST(Straight Tool ):
drill for general drilling.
MD(Micro Drill) :
Drilling pin with hole diameter below 0.4mm (inclusive)
For small aperture machining
SD(Slotting Drill):
For slotting
UC(Under Cut Drill):
Reducing the roughness of the hole wall and reducing the residual of Smear are characterized by the diameter below the head of the drill tip being smaller than the diameter above the head
ID(Inverse Drill):The drill needle with a diameter of 3.2mm or more and the drill tip angle of 165° are its special features.
2.Drill Bit Manufacturing Process
| Manufacturing process | Display | Detail |
| Tungsten carbide rod cutting |  |
Tungsten carbide rod cutting |
| Connect(PM) | 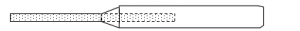 |
Welding of stainless steel shank and tungsten carbide drill with high frequency heating |
| Centerless grinding(一) |  |
Control shank diameter |
| Rough grinding and semi-precision grinding | 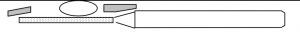 |
Grind the drill tip, shoulder and drill diameter to grind the drill diameter to close to the size |
| Fine grinding | 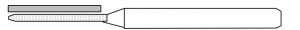 |
Grind drill diameter to specification |
| Centerless grinding(二) |  |
Control shank diameter and concentricity |
| Intermediate inspection |  |
Full inspection of drill bit diameter, taper, shank diameter, appearance concentricity and roundness |
| CNC Geometric cutting | 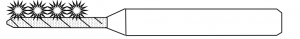 |
Cutting the groove, the drill tip surface |
| Wash | 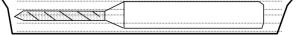 |
After ultrasonic cleaning, Automatic optical inspection (full inspection) |
| AOI Full inspection / packing |  |
Fully automatic optical inspection and packaging |
| FQC | OUT-OFF-BOX AUDIT |
3.Name Of Each Part Of Drill Bit


4.Judging standard for drill
Drill blade surface inspection

| Nth drill | Blade circle | |
| Diameter | 1411.56 |  |
| Fillet | 3.38 | |
| Gap | 1.45 | |
| Overlapping | 5.05 | |
| Split vertically | 0 | |
| Horizontally separated | 0 | |
| Bit eccentricity+ | 1.08 | |
| Big head | 0.38 | |
| small head | 0.42 | |
| Size Face | 2.55 | |
| Convex inside | 0.17 | |
| Outer arc hook | 0 | |
| Drill core thicknes | 219.19 | |
| Insufficient grinding |
| Size\Shape | Standard | Overlapping | Big head | Small head | Outer (inner) arc |
| Display |  |
 |
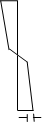 |
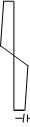 |
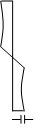 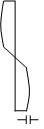 |
| 0.2~0.6 | 0 | 0.015D or less | 2°(0.015D) or less | 2°(0.015D)or less | 0.015D or less |
| 0.61~1.6 | 0 | 0.01D or less | 2°(0.015D)or less | 2°(0.015D)or less | 0.01D or less |
| 1.61~3.175 | 0 | 0.01D or less | 2°(0.015D)or less | 2°(0.015D)or less | 0.01D or less |
| 3.2~6.5 | 0 | 0.015D or less | 3°(0.02D)or less | 3°(0.02D)or less | 0.015D or less |
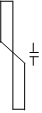
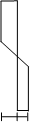
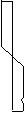
| Size\Shape | Separate | Eccentric | Large and small | Gap | Big side(small) |
| Display | 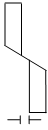 |
 |
 |
 |
 |
| 0.2~0.6 | 0.015D or less | 0.005 or less | A≧B≧4/5A | 30times 0.003or less | 1°or less |
| 0.61~1.6 | 0.01D or less | 0.010 or less | A≧B≧4/5A | 20times 0.005or less | 2°or less |
| 1.61~3.175 | 0.01D or less | 0.010 or less | A≧B≧4/5A | 10~8times 0.005or less | 2°or less |
| 3.2~6.5 | 0.015D or less | 0.020 or less | A≧B≧4/5A | 10~8times 0.008or less | 2°or less |
5.ST type,UC type structure advantages and disadvantages:
•ST
♦ Basically more regrind frequency than UC type
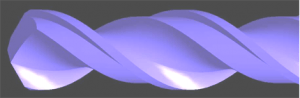
•UC
♦ The hole wall quality can be improved by reducing the area in contact with the substrate
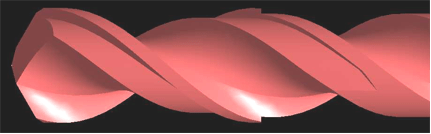
6.ST、UC Design advantages and disadvantages:

| UC design advantages | Design advantages and disadvantages |
| High-quality drilling quality, low drilling temperature, low nail head, glue residue, and breakage rate | Simple operation, easy diameter control, more grinding frequency |
| The low breakage rate reduces the drilling torque resistance. | Large range of use, used for general purpose |
| Conducive to micro-drills and PCB boards with more than 6 layers | It is good for general diameter drill bit, double face plate and multi face plate under 6 layers. |
7.ST、UCFever temperature


8.Differences in the design of drill core thickness

9.The difference of the design of the thick inverted cone of drill core

10.Differences in the design of drill-ditch flute

11.Differences in the design of the drill helix angle

12.Cutting conditions for drilling
■Spindle speed N: RPM
■infeed knife speed F: (Return knife speed RTR:)
■1m/min=16.7mm/sec =39.4IPM
■Chip Load f:
■F/N・1000 mm/rev.
■Number of holes etc..
13.heoretical cutting conditions
■ FR-4 DS V=200m/min
■ FR-4 MLB V=180m/min
■V=pDN/1000 V:(m/min)
■ p :
■ D:mm
■ N:R.P.M
14.Theoretical spindle number


15.Advantages of high-speed machining
■ The same of Chip Load, Quality tendency at different speeds

■ The same of Chip Load, Quality tendency at different speeds


■ The same of Chip Load, Processing time difference

■Selection of rotational speed:Not too high or too low

■Selection of infeed knife:Not too big or too small


■Selection of infeed knife:Not too big

■Abrasion: The relationship between bit wear and PCB layers

■Penetration of the lower plate
Penetration(DEPTH) = Penetrating part (L1) + length of front end of bit (L2)

(The tip angle is 130°)
16.The main factors affecting the quality of the drill bit

17.Requirements for drilling quality
■ Drilling deflection
■ Drilling wall thickness
■ Smear
■ Nail head
■ Breakage resistance
■ Chip removal and others
18.Drilling Deflection
■ Related projects

♦Drill rigidity
♦Appropriate number of plates
♦Spindle Run-out Management
♦Use of appropriate Entry Board
♦Drilling machine accuracy
19.Drilling accuracy(Shift)

■ Related projects
♦Incorrect positioning PIN
♦Drilling machine shift
♦Inner layer shift
20.hole roughness
■ Influences
♦The reliability of electrical conduction after electroplating
♦Reliability on inner insulation
■ Bit shape (the groove shape is connected))
♦Core thickness(Web)
♦Core thickness inverted cone(Web Taper)
♦Ditch ratio Ditch lengthBody Length)
■ Bit shape (shape related)
♦Helix angle
21.Resin Smear 
■ Phenomenon
♦Resin melted by heat during drilling
♦Attached to the inner copper foil
♦⇒Cause poor plating
■ Countermeasure
♦Reduce the area where the drill bit contacts the hole wall
♦Use UC
♦Speed up the infeed knife speed
♦No. of holes,No. of boards Re-examine
♦Implement go smear project
22.nail head
■ Phenomenon
♦When drilling, the inner copper foil can not be cut smoothly, but it can be stretched and stretched into a shape like a nail head


■Countermeasure
♦Reduce the area where the drill bit contacts the hole wall
♦Use UC Speed up the infeed knife
♦speed No. of holes,No. of boards Re-examine
23.ST and UC shapes
 Blade band at least 0.2mm remaining
24.Drill bit inspection items


■Overlap,Gap

■Primary Flare,Primary Taper

■Layback,Hook

■Offset ,Chisel point Inconcentricity


25.validation tools
♦Solid microscope: use the principle of optical magnification to magnify the drill bit for knife surface inspection Adjust magnification according to different drill diameters.
♦Tool microscope: Use the principle of optical magnification to magnify the drill bit for knife face inspection and measurement. The specific value of the knife face can be measured, and the inspection standard can be compared to judge the bit face of the drill bit.
26.The influence of poor cutting surface on drilling


27.Impact on Registration Accuracy: Heavy
♦Chisel point inconcentricity

28.Impact on Registration Accuracy: Medium
♦Overlap
